
On this page
- Diagnosis summary
- Safety and classification scope
- Classification & Scope (Normative)
- Typical Presentation (Informative)
- Field Identification Cues (Normative)
- Surface-catch class (MSRT)
- Visual signature
- Viewing / lighting
- Location / access
- Mechanism cue (context)
- Severity & CAT Mapping (Normative)
- Differentiation & Mis-ID Pitfalls (Informative)
- Evidence Package *(Documentation Requirements) (Normative)
- Reporting Language (Template)
- Related glossary terms
- Related DSS
- Source and version
DAMAGE SPECIFICATION STANDARD / METHOD-AGNOSTIC
DSS-Th.02.02 — Overheated Grinder/Belt Burn Line
Thermal + mechanical - friction heat band with gloss shift and possible shallow micro-texture
Diagnosis summary
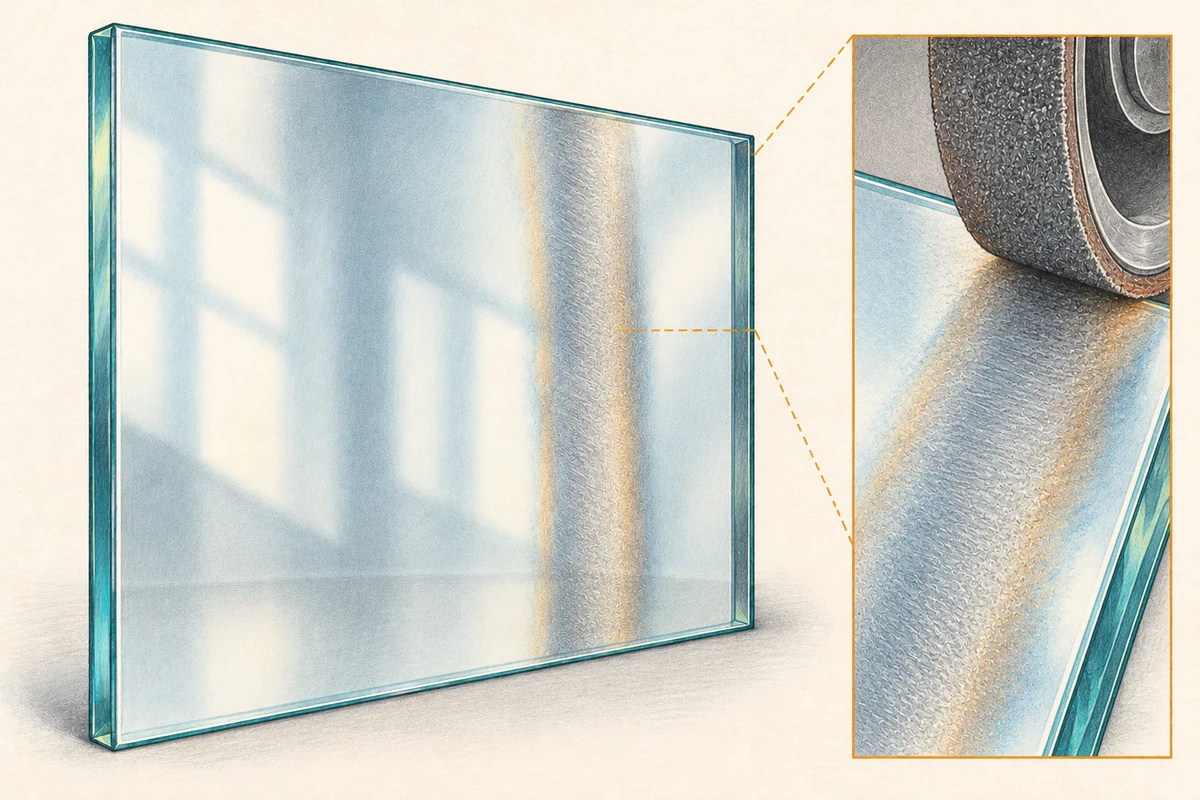
An overheated grinder/belt burn line is a localized, elongated band produced when a powered abrasive (grinder, belt, pad, or wheel) is run against the glass (often inadvertently) long enough to generate frictional heat. The result is a tone/shine shift (and, at higher severities, modeled micro-texture/matte) along the tool path. Classification is appearance-only per VIS (method-agnostic).
Classification & Scope (Normative)
NormativeAn overheated grinder/belt burn line is a localized, elongated band produced when a powered abrasive (grinder, belt, pad, or wheel) is run against the glass (often inadvertently) long enough to generate frictional heat. The result is a tone/shine shift (and, at higher severities, modeled micro-texture/matte) along the tool path. Classification is appearance-only per VIS (method-agnostic). Inspect after Non-Invasive Reveal under VIS lighting/geometry; record surface numbering and worked-surface status on Forms:
Typical Presentation (Informative)
Informative- Linear/curvilinear band tracking tool travel, sometimes with a feathered head/tail and central hot core.
- In specular view: duller gloss or color/contrast shift vs. adjacent glass; in raking light: non-directional, modeled micro-texture within the band.
- May show light residue (rubber/compound) that clears at reveal, leaving the core burn band visible.
Field Identification Cues (Normative)
NormativeSurface-catch class (MSRT)
- SC-0 when effect is optical only (gloss/tone shift without relief).
- SC-1 (slight) where very shallow micro-texture is present; SC-2 (clear) is uncommon but possible on severe overheats approaching frosted appearance. Perform one light, non-marring pass (polymer stylus if a coating is suspected). MSRT supports classification only.
Visual signature
- Continuous band with soft boundaries; no discrete pits/craters and no chip-flank sparkle typical of scoring.
- Texture inside the band reads modeled (non-directional), not a swirl/web of abrasive scratches.
Viewing / lighting
- Evaluate clean & dry at 12 / 36 / 72 in, normal incidence and oblique sweep (~60°-120°) with raking light to resolve any micro-texture; document distances/angles in-frame.
Location / access
- Record pane ID and surface numbering (#1-#4; laminate-internal). If parallax demonstrates a between-pane look-alike, classify CAT-5 by location and refer per project protocol.
Mechanism cue (context)
- Nearby evidence of powered abrasives (handheld grinders, belts, polishers), belt tracking marks on adjacent finishes, or compound/rubber smear at band edges.
Severity & CAT Mapping (Normative)
NormativeAssign CAT by appearance + MSRT + morphology (three-part cueing). Depth/relief values are indicative-no measurement required.
- CAT-1 (Benign/non-relief): Sheen/tone shift only; SC-0; visible primarily in raking at close/standard view. Indicative relief: ~0-10 μm (optical only).
- CAT-2 (Light): Subtle modeled micro-texture, SC-1; limited impact at standard view; boundaries remain soft. Indicative relief: ~10-40 μm.
- CAT-3 (Moderate): Clear detect (SC-2) with apparent modeled micro-texture at standard view; still no pits/craters, no chip flanks. Indicative relief: ~40-120 μm.
- CAT-4 (Severe): Pronounced matte/frosted lane from overheating/incipient devitrification; distinct at standard & wide-field views; no discrete pepper. Indicative relief: ~120-300 μm+.
- CAT-5 (by location/condition): Between-pane/inaccessible by parallax, integrity indicators (active cracks/pane movement), or confirmed coating-side loss on the surface to be worked → CAT-5.
CAT is appearance-based; acceptance is separate under VIS-A at 12/36/72 in. Do not use MSRT to “probe” or alter surfaces.
Differentiation & Mis-ID Pitfalls (Informative)
Informative- vs. Linear scoring (M.01): Scoring shows abrasive lines with chip-flank sparkle and SC-2 along edges; burn lines show modeled micro-texture/gloss shift with soft boundaries.
- vs. Torch proximity streak (Th.02.01): Torch bands align with a heat plume and may accompany soot films; belt/grinder burns track tool contact and often coincide with rubber/compound smears (removable).
- vs. Hot-particle peppering (Th.01.xx): Slag/sparks present discrete fused nodules or pits with bright rims; burn lines lack discrete pepper.
- vs. Residue films (R-family): Films clear at reveal and read SC-0; a persisting core band with SC-1/2 micro-texture indicates thermal burn.
- vs. Coating anomalies (Co-family): Coating rub/patchiness shows sheen/color change but - if on a worked coated surface - is not permitted at acceptance; confirm coating presence and apply VIS §6.2.e.
Evidence Package *(Documentation Requirements) (Normative)
Normative- Photo set (VIS): 12 / 36 / 72 in, normal + oblique, include raking macros resolving micro-texture within the band; add context frames showing tool path or nearby abrasive equipment. Record distance/angle in-frame.
- MSRT result: Record SC-class (SC-0/1/2) with one light, non-marring pass; polymer stylus on suspected coated faces.
- Forms: Pane ID; product family & surface numbering; worked surface Y/N; functional coating present on worked surface? (Y/N/Unknown); reveal status; lighting/time; geometry checklist; photos attached.
- Acceptance split: Post-restoration acceptance per VIS-A §6; classification ≠ acceptance. Coating-side anomalies on the worked surface remain disqualifying.
Reporting Language (Template)
Template- Th.02.02 Overheated Grinder/Belt Burn Line - Localized heat-affected band on surface #___ with [SC-0/SC-1/SC-2], no pits/craters or chip flanks; visible at [12/36/72 in] under VIS geometry after Non-Invasive Reveal. Morphology: sheen/contrast shift ± modeled micro-texture; boundaries soft. Classification: CAT-[1/2/3/4] by cues; CAT-5 if between-pane/integrity or coating-side loss on the surface to be worked. Forms + photo set attached; acceptance per VIS-A §6.
Related glossary terms
- AbrasiveGRK-168
- Raking lightGRK-129
- Coating rubGRK-115
- ScratchGRK-032
Source and version
GlassRenu Damage Specification Sheets (DSS), DSS-Th.02.02. Source revision and extraction date are recorded in the deployment manifest.
Open the complete published DSS with table of contents (PDF)
Normative and informative labels are preserved from the source. The downloadable one-sheet is a condensed classification aid; this web page retains the complete source-based specification content.