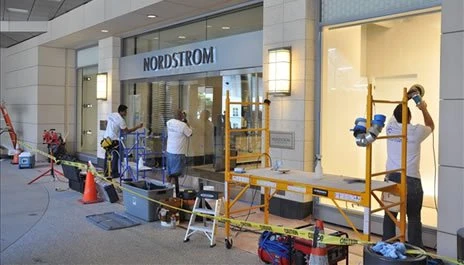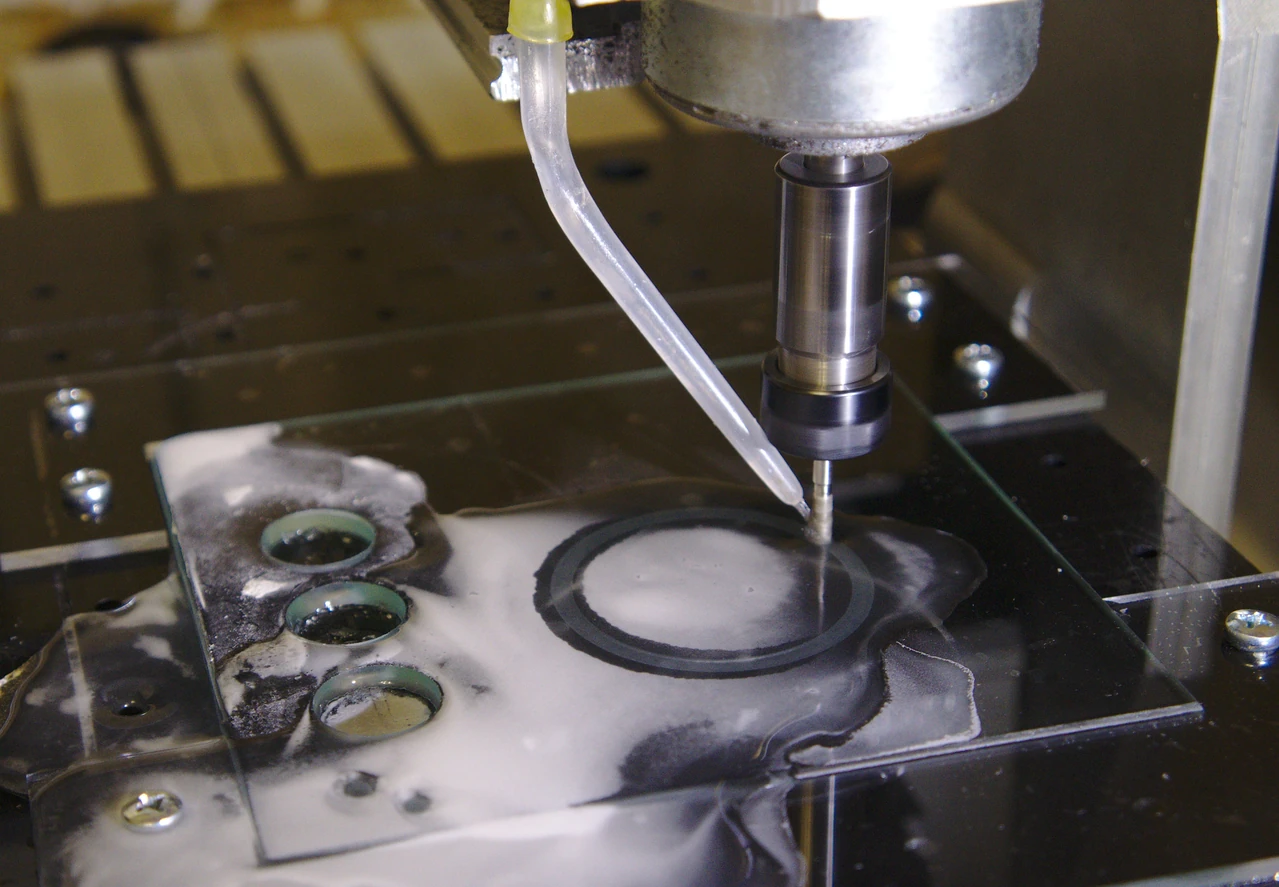
Wet process
A restoration or finishing operation performed with deliberately applied liquid at the tool-surface interface.
A restoration or finishing operation performed with deliberately applied liquid at the tool-surface interface.
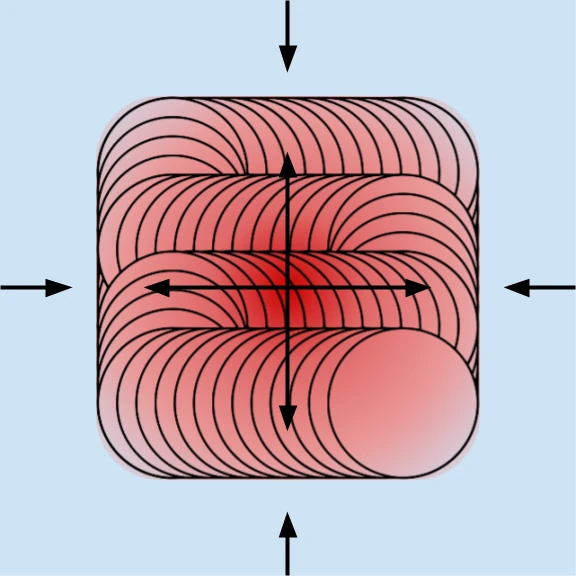
Production of thermal energy at the tool, pad, slurry, and glass interface through friction, deformation, fluid behavior, and machine losses.
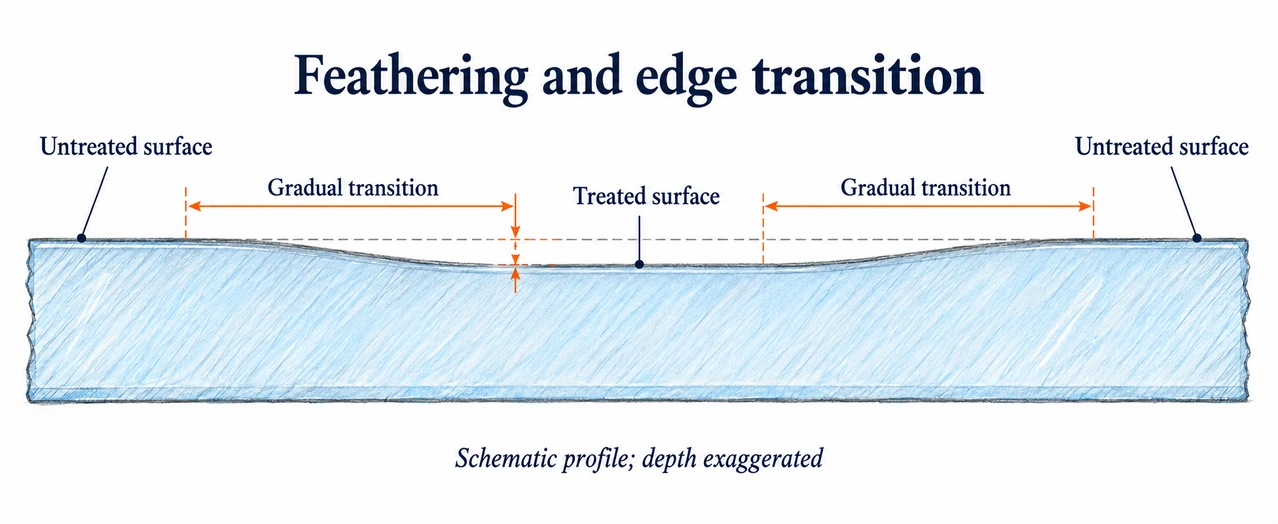
Progressively reducing treatment intensity toward the perimeter of a work area so the surface profile and finish merge gradually into untreated glass.
A compatible fluid used to remove heat, carry debris, reduce friction, improve particle transport, or stabilize the tool-surface interaction.
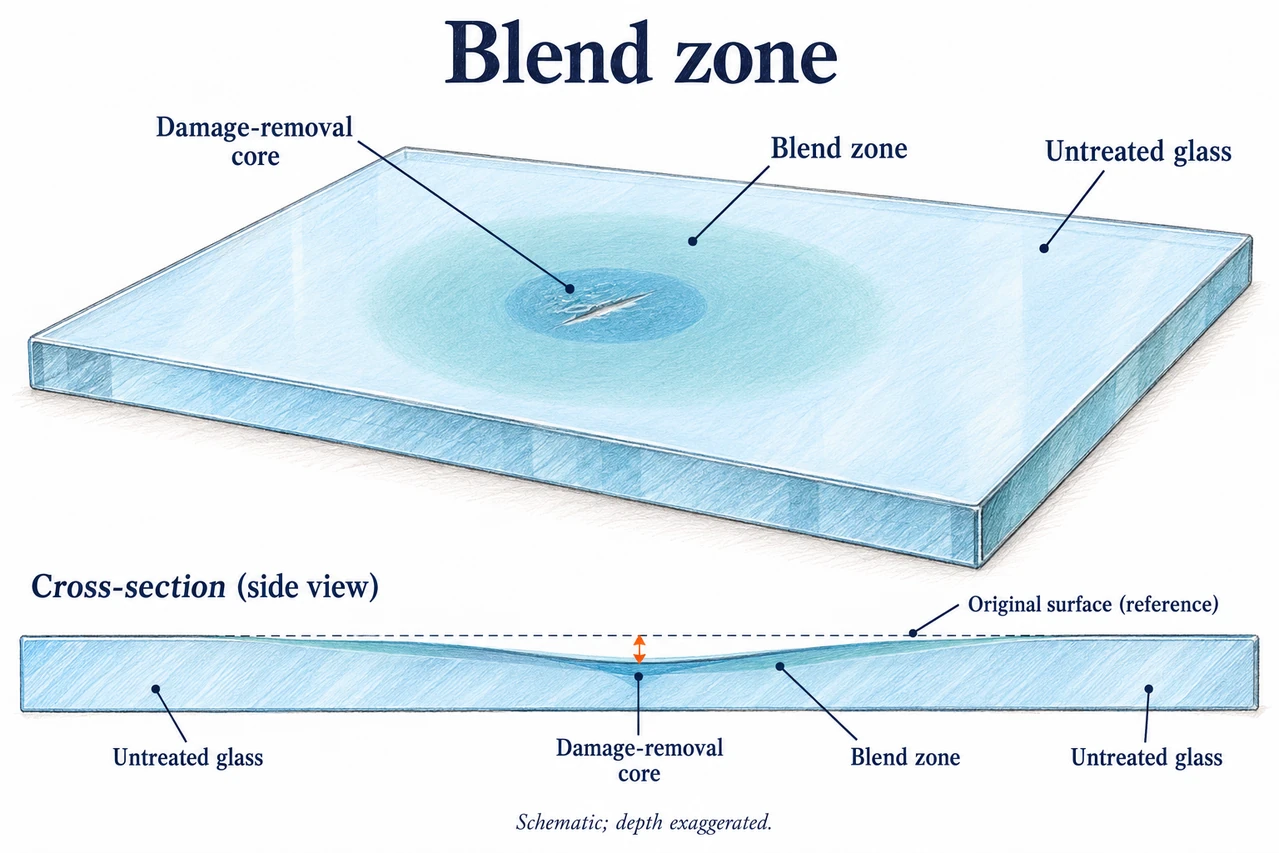
The surrounding area over which material removal or finishing is gradually distributed to transition from a deeper treated region into adjacent glass.
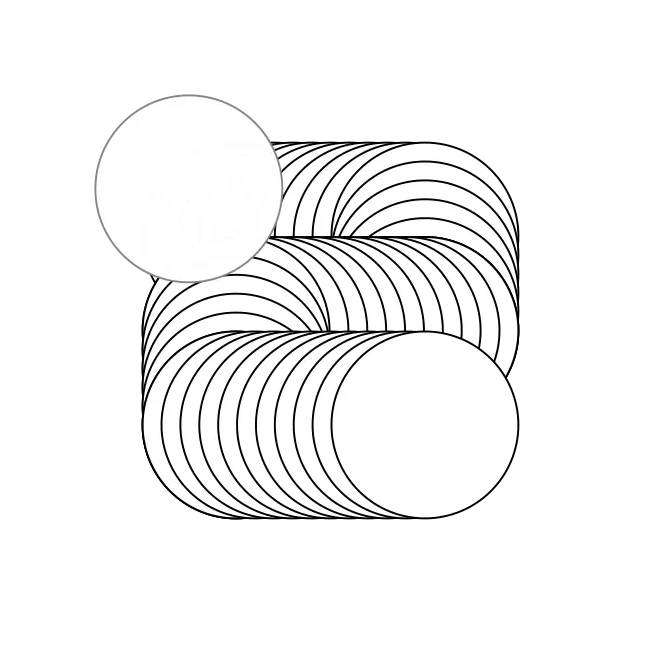
The portion of one tool path intentionally covered again by the next adjacent path, stated as a distance or percentage of working width.
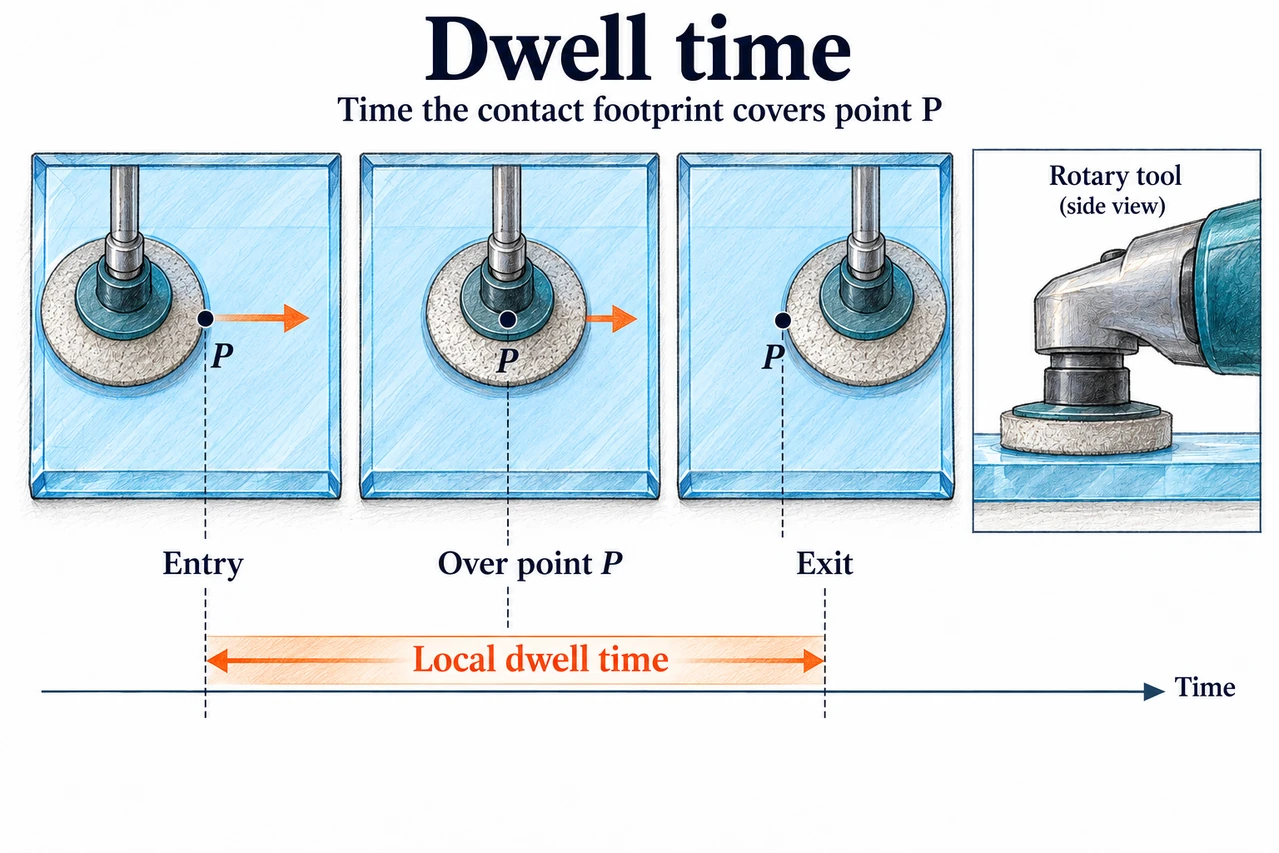
The time a moving or stationary tool acts on a particular location or defined area under stated process conditions.
One controlled traversal of the working tool across a defined path or area under stated settings.
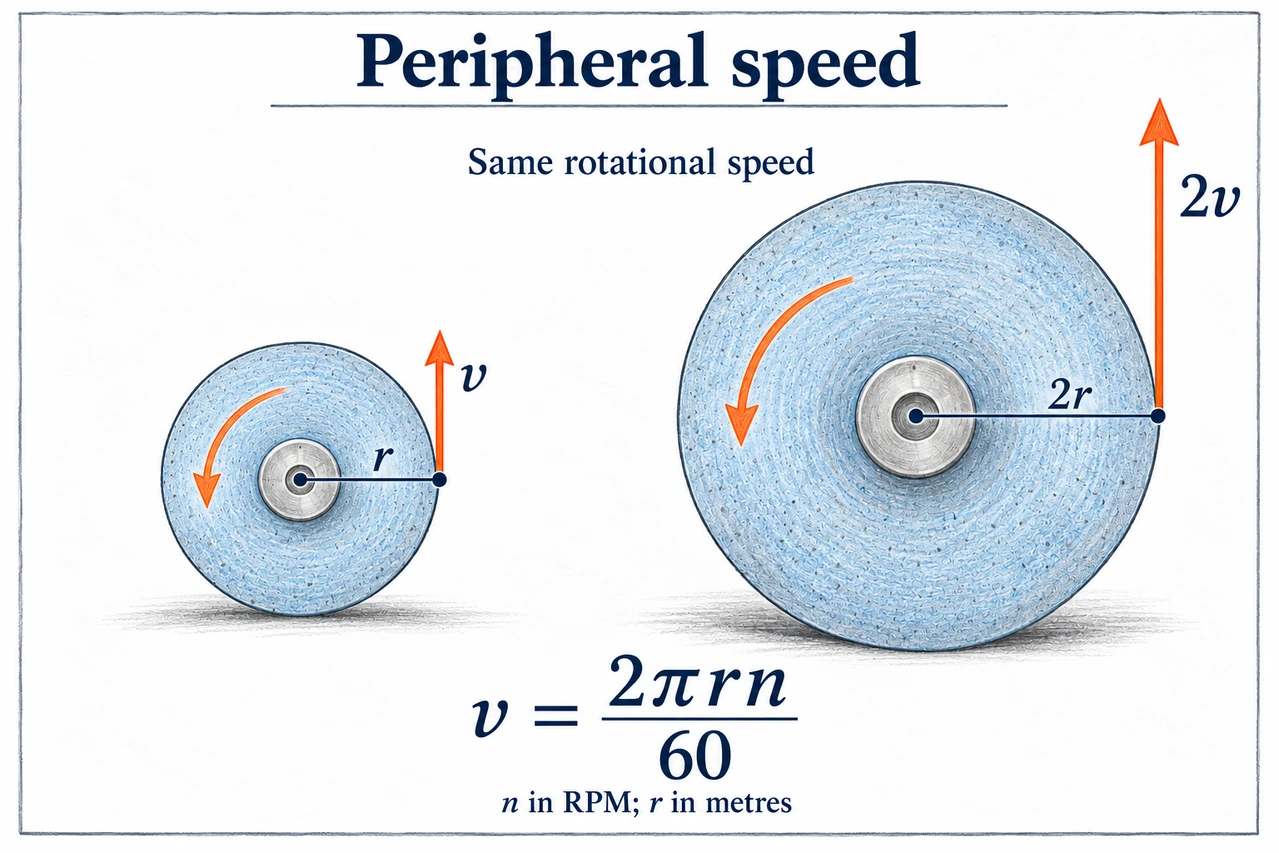
The linear speed of a point on the circumference of a rotating disc, determined by rotational speed and effective diameter.