
On this page
- Diagnosis summary
- Safety and classification scope
- Classification & Scope (Normative)
- Typical Presentation (Informative)
- Field Identification Cues (Normative)
- Surface-catch class (MSRT)
- Visual signature
- Viewing / lighting
- Location / access
- Mechanism cue (context)
- Severity & CAT Mapping (Normative)
- Differentiation & Mis-ID Pitfalls (Informative)
- Evidence Package (Documentation Requirements) (Normative)
- Reporting Language (Template)
- Related glossary terms
- Related DSS
- Source and version
DAMAGE SPECIFICATION STANDARD / METHOD-AGNOSTIC
DSS-Th.01.01 — Welding Slag Spatter (fused nodules/pits)
Thermal / hot-particle impingement - fused metallic droplets and resultant pits
Diagnosis summary
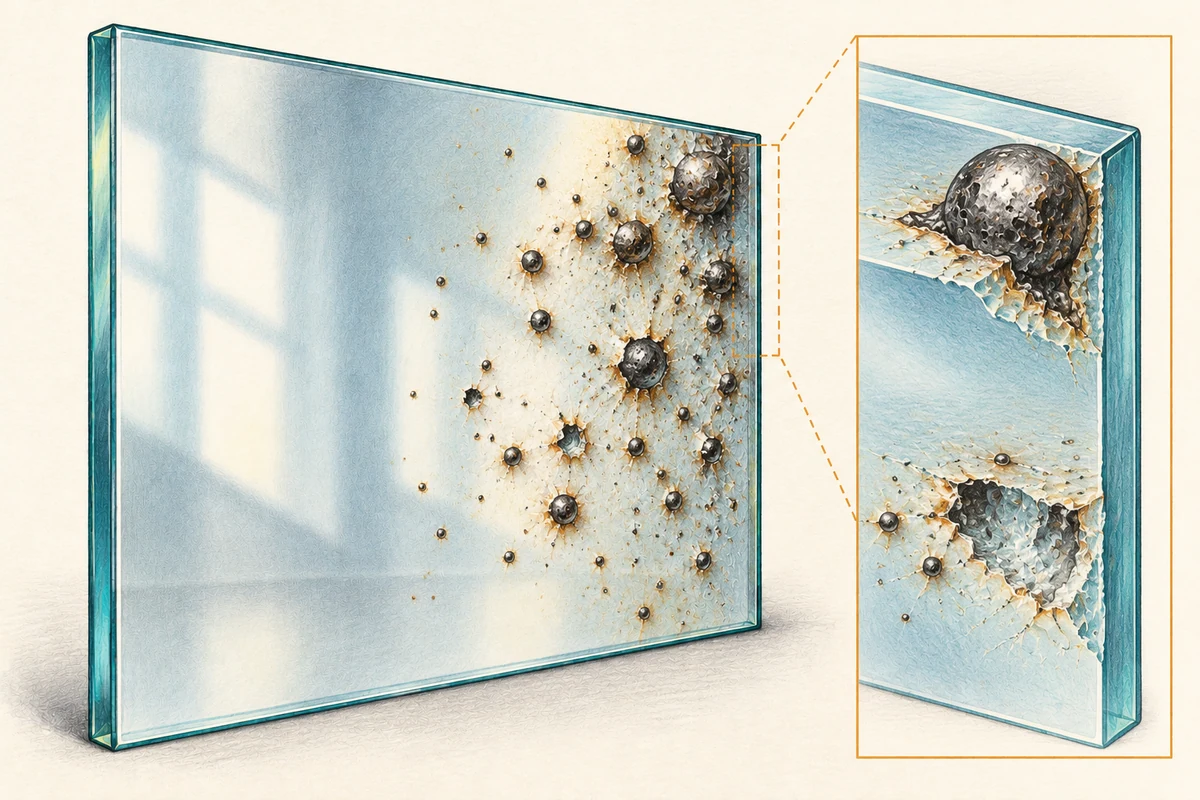
Welding slag spatter presents as fused metallic nodules and/or resultant pits/craters formed when hot particles (weld spatter) impact and partially fuse to the glass, often followed by detachment leaving a pitted field. Classification is appearance-only per VIS; methodology is out of scope. Inspect under VIS lighting/geometry after Non-Invasive Reveal;
Classification & Scope (Normative)
NormativeWelding slag spatter presents as fused metallic nodules and/or resultant pits/craters formed when hot particles (weld spatter) impact and partially fuse to the glass, often followed by detachment leaving a pitted field. Classification is appearance-only per VIS; methodology is out of scope. Inspect under VIS lighting/geometry after Non-Invasive Reveal; record surface numbering and worked-surface status on Forms: Use the Manual Surface-Relief Test (MSRT) only as a single, non-marring pass to confirm relief; it does not determine acceptance.
Typical Presentation (Informative)
Informative- Peppered field of dark or metallic specks; some remain proud/fused, others have detached, leaving bright, crater-like pits with halo in raking light.
- Often clustered on elevations adjacent to welding operations (balustrades, canopy frames, stair rails).
- May coexist with grinding sparks (ferrous “pepper”) and heat tinting on nearby metals.
Field Identification Cues (Normative)
NormativeSurface-catch class (MSRT)
- On fused nodules, a light, single pass typically yields SC-2 (clear); on detached pits, SC-1 to SC-2. Do not abrade; one non-marring pass only; polymer stylus if a coating is suspected.
Visual signature
- Discrete, high-contrast nodules (sometimes metallic sheen) and sharp-edged micro-craters; bright chip-flank sparkle at pit edges under raking.
- Fields may show directional bias toward the source; individual pits do not track as continuous lines (distinguishes from linear scoring).
Viewing / lighting
- Evaluate clean & dry at 12 / 36 / 72 in, normal incidence and oblique sweep (~60°-120°) using raking light to reveal relief.
Location / access
- Record pane ID and surface numbering (#1-#4; laminate-internal). If parallax or construction indicates a between-pane condition, classify CAT-5 by location (out of in-place scope).
Mechanism cue (context)
- Welding slag / grinder overspray is a typical origin for severe mechanical-thermal fields. (Informative linkage from VIS category notes.)
Severity & CAT Mapping (Normative)
NormativeAssign CAT by appearance + MSRT + morphology (three-part cueing). Numeric depth bands are indicative only-measurement is not required for classification.
- CAT-2 (Light): Sparse nodules/pits; SC-1 (slight) to SC-2 (clear) on a few features; visible mainly in raking at close/standard view. Indicative depth: ~20-60 μm (pit diameter typically ≤0.3 mm).
- CAT-3 (Moderate): Clustered field, numerous clear-catch pits with bright flanks; noticeable at standard distance. Indicative depth: ~60-150 μm; mixed nodules and detached pits.
- CAT-4 (Severe): Dense peppering / crater field, frequent fused nodules with rough micro-flanks, occasional micro-fracture lips at pit margins; visible at standard & wide-field. Indicative depth: ~150-400 μm+.
- CAT-5 (by location/condition): Between-pane cues, active cracks, pane movement, or coating-side loss on the surface to be worked → CAT-5 (non-repairable/out of in-place scope).
CAT is appearance-based; acceptance is separate and governed by VIS §6 at 12/36/72 in under defined conditions.
Differentiation & Mis-ID Pitfalls (Informative)
Informative- vs. Grinder spark embed (Th.01.02): Grinder pepper tends to be finer, more uniform; welding slag shows larger, irregular nodules/pits with higher local energy signatures.
- vs. Sand abrasion (E.02.01): Eolian matte is broad, directional micro-texture (field haze) rather than discrete fused droplets.
- vs. Coating anomalies (Co.01/Co.03): Coating rub/patchiness lacks fracture facets/pits and shows sheen/color shifts rather than fused bodies; also governed by coated-surface acceptance rules on the worked surface.
- vs. Linear scoring (M.01): Scores form continuous tracks; slag presents as discrete peppering without long run-length.
Evidence Package (Documentation Requirements) (Normative)
Normative- Photo set (VIS): 12 / 36 / 72 in; normal + oblique; include raking macros resolving facet/halo at representative pits and at least one context frame showing proximity to weld source. Record distance/angle in-frame.
- MSRT result: One light, non-marring pass on a representative nodule/pit; SC-class = SC-1/SC-2 as observed; polymer stylus where a coating is suspected.
- Forms: Pane ID; product family & surface numbering; worked surface Y/N; functional coating present on worked surface? (Y/N/Unknown); reveal status; lighting/time; geometry checklist; photos attached.
- Acceptance split: Post-restoration acceptance per VIS §6 at 12/36/72 in; classification ≠ acceptance. Coating anomalies on a worked coated surface remain disallowed at acceptance per VIS §6.2.e.
Reporting Language (Template)
Template- Th.01.01 Welding Slag Spatter - Discrete fused nodules / pits on surface #___ documented at 12/36/72 in, normal + oblique with raking; MSRT = SC-[1/2] on representative features. Morphology shows peppered field with crater halos; no continuous linear scoring observed. Classification: CAT-[2/3/4] by density and relief; CAT-5 if between-pane, active cracks, or coating-side loss on the surface to be worked. Forms + photo set completed; acceptance per VIS §6 (separate).
Related glossary terms
- Welding slagGRK-100
- Weld spatterGRK-068
- Raking lightGRK-129
- Coating rubGRK-115
- AbrasionGRK-035
- GrindingGRK-166
Source and version
GlassRenu Damage Specification Sheets (DSS), DSS-Th.01.01. Source revision and extraction date are recorded in the deployment manifest.
Open the complete published DSS with table of contents (PDF)
Normative and informative labels are preserved from the source. The downloadable one-sheet is a condensed classification aid; this web page retains the complete source-based specification content.